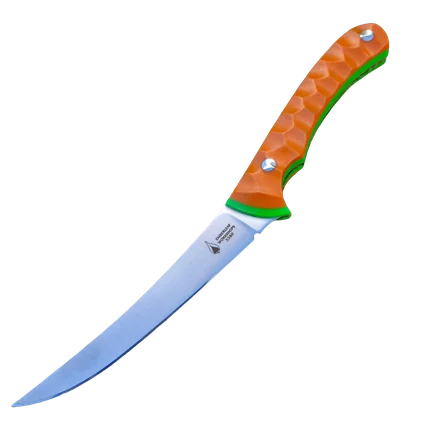
The making of a knife
How an Emberleaf knife is made
By hand, in our workshop in Petworth, West Sussex: from the steel blank to the stitched sheath, in eight stages.
One workshop, one maker’s mark
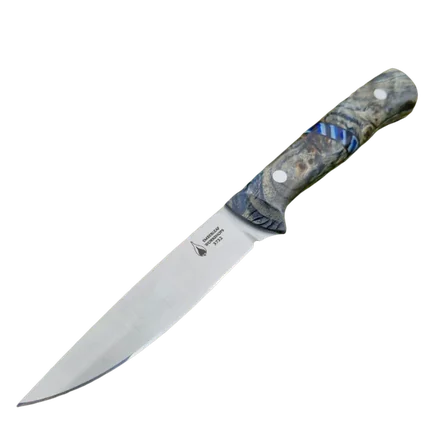
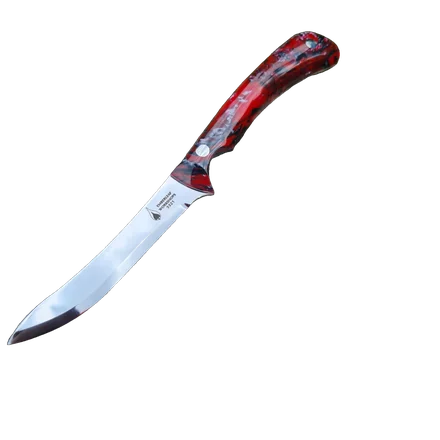
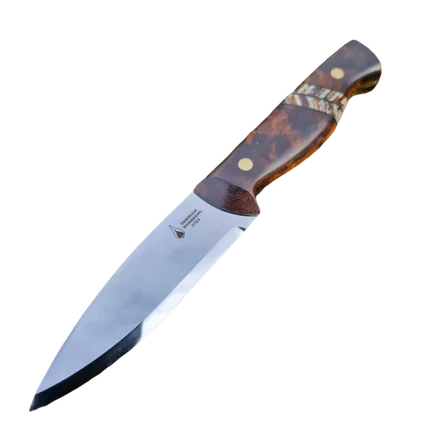
Emberleaf was founded in 2012 by Dean Boyd and Joel Andreas, two former Royal Engineers, and more than five thousand knives have left the Petworth workshop since. The steel arrives as a cut blank. Everything after that, heat treatment included, is done here.
Knifemaking in England has been a regulated craft since the Cutlers’ Company was established in 1624, and a maker’s mark has always meant that someone answers for the blade. Every Emberleaf blade carries ours, with its own project number. More on the English tradition.
- Founded
- 2012
- Knives made
- 5,000+
- Workshop
- Petworth, West Sussex
The eight stages
Receiving · profile
Steel arrives, cut to profile
We don’t forge the bar. Mill-rolled tool steel and Damascus billets come in pre-cut to the knife’s outline — waterjet through the rough shape, drilled where the pin holes need to land. From here on, every hand on the blade is ours.
Watch this stage, 0:30Belt grinder · PAPR booth
Grind the bevels
Heavy stock removal on the belt grinder, in PAPR with full extraction. Bevels, distal taper, the curve of the spine — judged by eye and ground in by hand against the platen, pass after pass.
Watch this stage, 0:44Heat-treat · in-house
Wrap, soak, quench
The blade goes into a stainless-foil pouch and into the kiln to soak at austenitising temperature. Out of the foil, straight into the oil quench — the flash of flame is the carbon shifting state. Tempered the next day to spec hardness.
Watch this stage, 1:14Etch tank
Bring the pattern up
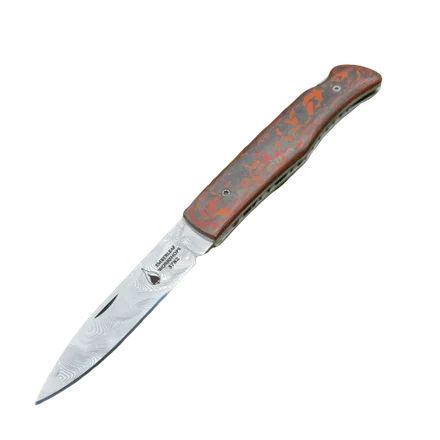
For Damascus, the pattern is locked in the steel before we start — but you only see it after the etch. Mask everything that isn’t blade, dip in ferric chloride, neutralise, repeat until the contrast is right. The hard layers stand proud; the softer ones recede.
Watch this stage, 2:57Handle bench
Build the handle
Handle scales — burl, dichrolam, micarta, mammoth — are drilled to match the tang, then bonded with two-part epoxy and pinned. Bolsters fit flush against the ricasso. Clamped, set, given a day to cure before they go anywhere near a grinder.
Watch this stage, 3:56Belt grinder
Shape the handle
Handle blocks come off the bench rectangular. The shape is ground in — palm swell, pommel curve, finger relief — first with coarse grit on the belt grinder, then refined on the slack belt, then by hand. Wood and steel meet flush at the bolster line.
Watch this stage, 4:41Laser bench
Mark with the laser
The maker’s mark is laid into the ricasso with a fibre laser — Emberleaf logo, project number, steel call-out. A small, permanent stamp that says this one came out of this workshop, with this serial.
Watch this stage, 5:55Leather bench
Stitch the sheath
Every fixed-blade leaves with a sheath cut, bevelled, glued and stitched in the same workshop. Veg-tan leather, hand-marked from a pattern, contact-cemented at the seam, then stitched on the heavy machine and burnished at the edge. Made to fit the blade it ships with.
Watch this stage, 6:09
Closer looks
Single jobs from the bench, filmed at length.
Making a leather sheath
The hybrid sheath
Cutting the jimping by hand
The linisher, talked through
What leaves the workshop
Every finished knife carries its project number, etched on the blade and logged at the bench: model, steel, handle material and the year it was built. The number ties the knife to its record for as long as it is in use. Owning an Emberleaf.
The rooms themselves are on the workshop tour.